Manufacturing is at the forefront of innovation with the emergence of Industry 4.0 and widespread digitisation. The sector has displayed remarkable resilience emerging out of the pandemic’s shadow. However, factors such as inflation, economic instability, and geopolitical disturbances have made it difficult to conduct business today. Additionally, manufacturing industry problems, such as lack of skilled personnel, supply chain issues, manufacturing challenges and digitisation and automation challenges, can slow down the sector’s growth. To truly understand the challenges in manufacturing products today, we must explore these factors in detail. Let’s understand the challenges manufacturing industries face and how to overcome them.
Common challenges in manufacturing industry
The upswing in the manufacturing sector is an encouraging sign of the industry’s growth. However, several internal challenges in the manufacturing industry impede its growth. When asking, "what is the challenge in manufacturing products?" one of the most pressing concerns is labour shortage. Let’s delve into the most common manufacturing industry problems and their solutions.
Labour shortage
The manufacturing industry faces the challenge of finding the right people for the right job. In countries such as the USA, a large chunk of the workforce is approaching retirement age, adding to an already tightening talent pool. A recent industrial outlook survey pointed out that retaining high-performing talent was a top challenge.
Businesses can address the labour challenges in manufacturing through various measures such as pay raises as well as upskilling and reskilling staff through continuous training, which is a manufacturing challenge. Manufacturers can modify existing shifts to create flexible work arrangements, such as hybrid working. Moreover, the sector can tie-up with universities to raise awareness about jobs in the manufacturing industry. By improving health and safety standards in manufacturing, businesses can attract better talent and retain a high-skilled workforce.
Poor inventory and supply chain management
As supply chains continue to bear the brunt of global changes, supply chain disruptions and inventory control have emerged as significant problems facing the manufacturing industry. Manual stock checks are ineffective and prone to mistakes, leading to errors, shortages, excesses, and unidentified losses.
As a manufacturer, you must ensure suppliers’ stock reliability and quality management to maintain a successful manufacturing operation. Moreover, production and inventory management requires real-time tracking of goods and logistics to enhance quality control. All these aspects create a multi-layered complex supply chain. Deploying automated inventory management and improving end-to-end supply chain visibility leads to a smoothly functioning supply network. Using cloud-based, IoT, and AI-led systems can help with the real-time tracking of goods, collaboration, and seamless communication.
Lack of demand forecasting
A significant challenge in manufacturing industry processes is that they do not have enough reporting systems to predict sales in the coming months or years. As a result, they cannot fulfil commitments causing customer dissatisfaction, and ultimately, lower revenue for manufacturing companies. A lack of demand forecasting in manufacturing also affects budgeting and finance, production capacity building, inventory management, and sourcing and procurement.
Predictive analysis of consumer data helps businesses to accurately forecast demand and streamline manufacturing the product life cycle from the factory to the consumer. Advanced tools and software use relevant data to predict and prepare your business for future manufacturing industry trends in the short and long terms. Moreover, such analysis identifies inefficiencies in the production process and provides solutions.
Introducing automation
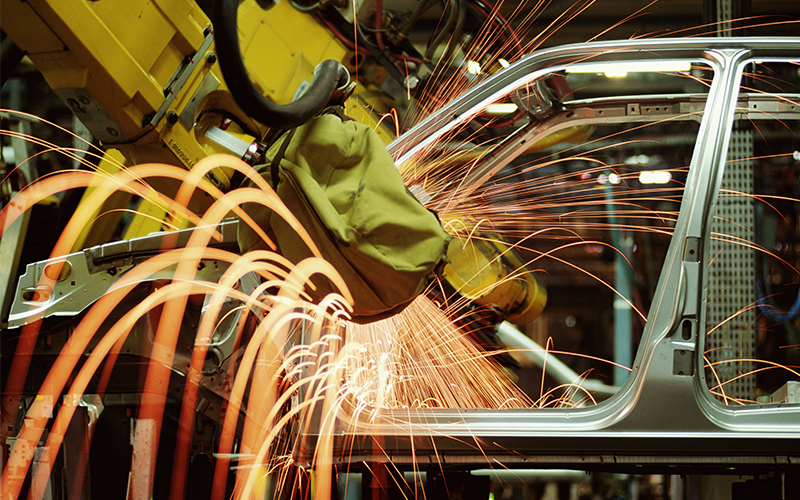
Choosing suitable systems to improve operational efficiency in manufacturing is always a task as it involves investing in technology and human resources. Investing in automation and robotics demands significant expenses besides generating a scare about job losses. Moreover, a lack of awareness about digital transformation in manufacturing and reliance on legacy systems create obstacles for manufacturers to compete with those actively using the latest technologies such as cloud, IoT, and AI.
The benefits of automation in production far outweigh the initial expenses. There is great potential in using new technology to solve the problems of manufacturing industries. Moreover, through effective change management, businesses can upskill the staff as automation replaces their work. This strategy can reduce the talent gap. By embedding technologies such as IoT in manufacturing, businesses can get real-time data on the production process and even machinery maintenance.
Operational inefficiency
Improving operational efficiency is one of the common manufacturing challenge problems in the industry. Businesses are looking for cost-effective and time-saving techniques to cut costs and increase the productivity of their operations. Furthermore, risk management is essential for long-term success in manufacturing, and a lack of insight can create obstacles to growth.
With the help of enterprise resource planning (ERP) solutions, the manufacturing industry can increase efficiency by modernising procedures and systematising workflows. Advanced ERP systems minimise time-consuming and labour-intensive operations, eliminate material waste, enhance equipment use by reducing damage, and simplify supply networks. Moreover, a robust risk management tool improves product and process quality continuously.
Growing ROI
The idea of a business is to enhance the return on investment (ROI), but this is a real challenge faced by the manufacturing industry. A great product will lie in the warehouse without efficient sales management, impacting the entire manufacturing process. Merely setting sales targets cannot boost sales. It requires a complete understanding of customer needs and buying trends. With CRM systems, businesses can identify their customer profile and buying patterns. This data also aids in efficient lead management, translating to sales for manufacturing companies.
Cybersecurity and data security
As manufacturing plants connect more equipment to the internet through IoT sensors, cloud platforms, and interconnected supply chain systems, they also become a bigger target for cyberattacks. A single compromised system can halt production, expose proprietary designs, or disrupt the wider supply chain, and manufacturing's growing reliance on operational technology (OT) alongside traditional IT makes it harder to secure everything with one approach.
Manufacturers can reduce this risk by segmenting IT and OT networks, applying consistent access controls and monitoring across both, and building cybersecurity into how new equipment and software are evaluated rather than treating it as an afterthought. Regular staff training also matters, since many breaches start with a simple phishing email rather than a sophisticated exploit.
Sustainability and regulatory compliance
Environmental regulations are tightening across major manufacturing markets, and customers, investors, and partners increasingly expect visibility into a manufacturer's environmental footprint, from energy use and emissions to how materials are sourced and disposed of. Meeting these expectations while still controlling costs is a genuine balancing act, especially for manufacturers running on legacy equipment that wasn't designed with efficiency or emissions in mind.
Manufacturers are addressing this by tracking energy and resource use at the production-line level, prioritising efficiency upgrades that pay for themselves through lower operating costs, and building sustainability reporting into existing quality and compliance processes rather than running it as a separate initiative.
For organisations on the digital transformation journey, agility is key in responding to a rapidly changing technology and business landscape. Now more than ever, it is crucial to deliver and exceed organisational expectations with a robust digital mindset backed by innovation. Enabling businesses to sense, learn, respond, and evolve like living organisms will be imperative for business excellence. A comprehensive yet modular suite of services is doing precisely that - equipping organisations with intuitive decision-making automatically at scale, actionable insights based on real-time solutions, anytime/anywhere experience, and in-depth data visibility across functions leading to hyper-productivity, Live Enterprise is building connected organisations that are innovating collaboratively for the future.
How can Infosys BPM help solving manufacturing industry challenges?
Infosys BPM offers comprehensive business options tailored to business process in manufacturing industry. From labour and supply chain challenges to the cybersecurity and sustainability pressures covered above, addressing manufacturing industry problems increasingly means combining process expertise with the right technology and reporting discipline. Our centre of excellence draws on the knowledge of professionals in related fields and business consultants to provide innovative solutions for our customers.
Frequently asked questions
The most common manufacturing industry challenges are labour shortages, supply chain and inventory management problems, a lack of demand forecasting, the cost and complexity of introducing automation, operational inefficiency, cybersecurity risk as plants become more connected, and pressure to meet sustainability and regulatory requirements. Most manufacturers face several of these at once.
Manual stock checks are the root cause in most cases; they're slow and error-prone. Replacing them with automated inventory management and real-time, end-to-end supply chain visibility, often using cloud, IoT, and AI-led tracking, is the most common fix, since it catches shortages, excesses, and losses before they affect fulfilment.
As manufacturing plants adopt more connected equipment, IoT sensors, and cloud-based systems, they create more entry points for attackers, and a single breach can halt production or expose proprietary designs. It's a growing concern because manufacturing's operational technology often wasn't originally built with cybersecurity in mind, unlike standard IT systems.
Sustainability has moved from a nice-to-have to an expectation: regulators, investors, and customers increasingly want visibility into a manufacturer's energy use, emissions, and materials sourcing. Manufacturers that build sustainability tracking into existing production and compliance processes tend to manage this more cost-effectively than those treating it as a separate, bolted-on initiative.
Automation directly addresses several of the challenges above at once: it reduces reliance on scarce manual labour, gives real-time visibility into production and machinery health, and cuts the operational inefficiencies that come from manual, disconnected processes. The upfront investment and change-management effort are real, but they're generally outweighed by the efficiency and data-visibility gains over time.